Views: 0 Author: Site Editor Publish Time: 2026-11-20 Origin: Site
In the fiercely competitive plastics manufacturing sector, uneven cell structure directly threatens your bottom line. Factory managers frequently face increased scrap rates, compromised mechanical strength, and severe margin erosion due to inconsistent output. Pinpointing the root cause of these density fluctuations requires deep technical insight. You must evaluate both your raw material formulations and mechanical hardware capabilities simultaneously. Simply adjusting a single machine parameter rarely solves the overarching issue. This comprehensive guide provides a realistic, evidence-based framework for identifying core production bottlenecks. We will help you understand the delicate balance between thermal management, blending precision, and extrusion mechanics. You will learn exactly how to determine if minor process optimizations can solve your current operational challenges. Ultimately, we clarify when upgrading machinery becomes the only viable path to reliable product quality.
Hardware degradation is a primary culprit: Wear in the extruder screws or misaligned die heads directly causes flow imbalances and localized density variations.
Mixing uniformity dictates foaming consistency: Inadequate dispersion during the blending phase prevents uniform cell growth, regardless of extruder quality.
Thermal management is non-negotiable: Minor fluctuations in melt temperature or calibration cooling lead to premature or delayed foaming.
Strategic equipment evaluation: Resolving persistent density issues often requires auditing the entire production line, from raw material handling to downstream calibration.
Density variations create immediate roadblocks for market acceptance. Heavy edges and hollow centers severely compromise panel integrity. These physical flaws disqualify boards from premium PVC foam board applications like precision cabinetry, CNC routing, and high-end signage. Cabinet makers require absolute dimensional stability. CNC operators cannot mill panels containing inconsistent internal voids. High-end signage demands a flawless surface finish for direct digital printing. When your panels exhibit localized density shifts, premium buyers will reject the shipments entirely.
Defining clear success criteria prevents these costly rejections. Most commercial building compliance standards mandate strict uniformity. Acceptable density tolerance levels typically hover around ±0.02 g/cm³. Maintaining this tight tolerance ensures predictable mechanical strength across the entire board surface. Consistency guarantees reliable screw-holding capacity and optimal bending strength. Factory managers must establish these benchmarks early. You cannot manage production effectively without measuring output against rigorous, quantifiable standards.
Financial impacts often remain hidden until quarterly audits. Over-packing represents a massive stealth expense. When operators over-pack the die to eliminate voids, they consume excessive raw PVC resin. This practice wastes expensive material and destroys profit margins. Conversely, under-packing causes catastrophic structural failures. Flimsy boards fail structural integrity tests. Customer returns skyrocket. You must absorb the cost of return shipping, material scrap, and lost client trust. Balancing this equation demands precise control over your entire manufacturing operation.
Mechanical degradation directly drives foaming inconsistencies. Machinery dictates melt pressure, and pressure governs cell expansion. We can break down these mechanical components into three core solution categories:
Material feeding and plasticization zones.
Melt pressure generation mechanisms.
Die head distribution and shaping dynamics.
Screw and barrel wear represent the most common points of failure. Degraded twin screws cannot generate consistent shear. Plasticization drops when screw flights lose their sharp edges. Poor shear prevents uniform foaming agent activation. The blowing agent requires exact pressure and friction to decompose correctly. When screws wear down, material slips backward over the flights. This slippage creates pressure surges. Pressure surges manifest directly as alternating high and low-density bands across the finished board.
Die head dynamics play an equally critical role. T-die design determines how the melt spreads before exiting the lips. Improper choker bar adjustments restrict material flow unevenly. If an operator tightens the center choker bar excessively, the material forces its way to the edges. This causes heavy, dense edges alongside a weak, hollow center. Lip gap inconsistencies also provoke immediate edge-to-center density disparities. You must calibrate the die gap using precise feeler gauges during maintenance shutdowns.
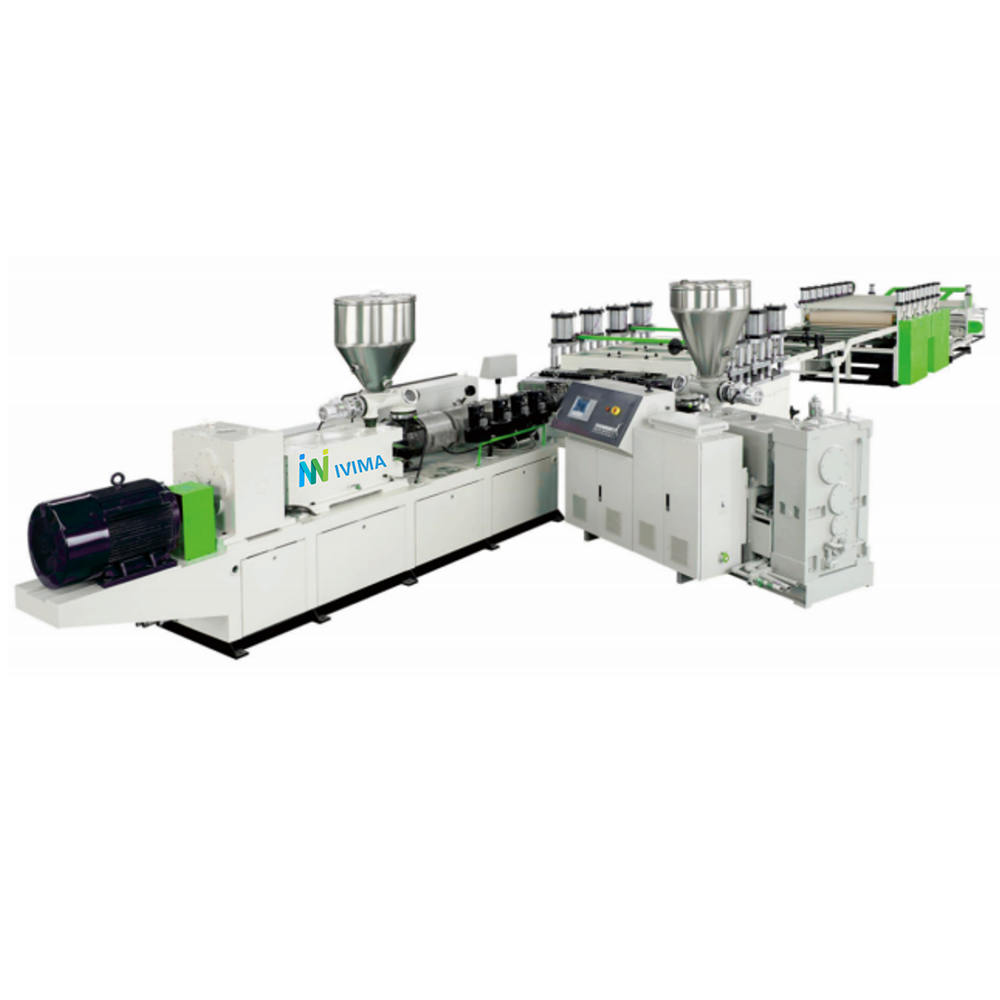
Determining the exact failure point requires careful evaluation. You must decide if a density issue stems from a simple calibration error on an existing PVC foam board extrusion line or permanent hardware death. Replacing a die lip costs significantly less than buying a new twin-screw barrel. Conduct a thorough teardown inspection to measure screw clearance against manufacturer specifications.
Observed Defect Symptom | Likely Hardware Cause | Likely Process Cause |
|---|---|---|
Heavy edges, hollow center | Improper choker bar adjustment | Center die temperature too high |
Longitudinal density waves | Worn extruder screw flights | Inconsistent powder feeding rate |
Random localized voids | Scratched or damaged die lip | Poor blowing agent dispersion |
Overall density too high | Insufficient barrel heating capacity | Excessive raw material over-packing |
Raw material preparation serves as the absolute foundation of density control. Extruders cannot fix poorly mixed powder. Formulations rely on complex chemical interactions. You must blend base resin, blowing agents, regulators, and stabilizers flawlessly. If the initial mixture lacks homogeneity, the final board will inevitably fail.
Dispersion realities dictate the success of the foaming process. Blowing agents like Azodicarbonamide (AC) and Sodium Bicarbonate (NC) release gas upon heating. Acrylic processing aids (ACR) wrap around these gas bubbles to prevent them from bursting. Poor dispersion of these chemicals creates localized hot spots. An excessive concentration of AC powder in one section causes violent over-foaming. A lack of ACR in another section causes the bubbles to collapse. These microscopic failures merge to form massive density variations visible to the naked eye.
Conducting a rigorous equipment audit prevents blending disasters. You must evaluate specific criteria for any PVC powder mixing machine operating in your facility. Pay close attention to these vital inspection points:
Blade wear: Worn deflector blades fail to create the necessary vortex, leaving additives at the bottom of the drum.
Cooling mixer efficiency: Inadequate cooling jackets allow the hot mixture to agglomerate before discharge.
Automated discharge accuracy: Faulty thermocouples dump the batch at incorrect temperatures, altering the bulk density of the powder.
Implementation risks run high when combining new recipes and old machinery. Running high-end, complex foaming formulations through outdated mixing equipment guarantees failure. The poor dispersion will result in staggering scrap rates. Material investments quickly disappear when the blending phase cannot support the chemical requirements. Upgrade your mixing infrastructure before purchasing expensive imported blowing agents.
Thermal management dictates the physical expansion of the panel. You must carefully map out the thermal journey of the PVC melt. The process typically fails at transitional checkpoints. The plastic transitions from solid powder to a viscous melt, then expands into a foam, and finally freezes into a rigid board. Any thermal disruption during these phases ruins the cell structure.
Extruder zone temperatures require a delicate, precise balance. You must manage the feeding, compression, and metering zones meticulously. If the feeding zone runs too hot, the powder bridges and blocks the intake. If the compression zone runs too hot, the blowing agent activates prematurely inside the barrel. Premature gas release forces the gas backward out of the vacuum port. This leaves no gas for actual panel expansion at the die exit. Conversely, cold metering zones create un-melted resin particles. These solid particles tear through the expanding foam structure like microscopic bullets.
Calibration board cooling shapes the final density profile. The calibration unit uses chilled water and vacuum pressure to pull the hot foam into its final dimensions. Uneven cooling water flow creates severe problems. Blocked vacuum channels cause the board's surface to freeze unevenly. When one side cools faster than the other, the internal core shifts. The softer, hotter material migrates toward the warmer side. This migration forces internal density shifts and warps the board entirely.
Adopt an evidence-oriented troubleshooting approach. Never rely on point-in-time assumptions or single readings. We highly recommend logging melt pressure and temperature deltas over a full 24-hour shift. Continuous data logging identifies slow thermal drift. A dying heater band might drop three degrees every hour. You will not notice this drift during a quick spot check. Data logging exposes these hidden hardware failures before they generate tons of scrap.
Capital expenditures require rigorous justification. Production managers must utilize a clear decision-stage framework. You face a critical choice: retrofit existing lines or invest in entirely new machinery. Retrofitting makes sense when the core extruder frame remains structurally sound. Buying a new die head or replacing a worn screw offers a cost-effective temporary fix. However, retrofitting cannot solve fundamental capacity limits or outdated control architectures.
Scalability and automation differentiate legacy setups from modern machinery. Modern plastic board production equipment mitigates density issues through advanced automation. Automated gravimetric dosing eliminates human error. It weighs additives continuously and adjusts feeding rates instantly based on extruder RPM. Closed-loop temperature control systems monitor melt heat continuously. They trigger cooling fans or heater bands automatically to maintain a strict ±1°C tolerance. These automated interventions stabilize the foaming environment entirely.
Vendor evaluation determines long-term operational success. Do not accept vague promises during the procurement phase. Demand strict, quantifiable guarantees from equipment manufacturers. Require guaranteed output tolerances written into the final contract. Force the vendor to conduct performance testing using your specific proprietary formulation. Refuse the machinery if it fails to hit the ±0.02 g/cm³ benchmark during factory acceptance tests. Additionally, verify regional technical support capabilities. A broken machine holds no value if replacement parts take three months to arrive.
Execute structured next-step actions before signing purchase orders. Guide your production managers through a rigorous Design of Experiments (DoE) protocol. A structured trial run isolates individual variables systematically. First, test a brand-new formulation on the old machine. Next, test the old formulation using varied temperature profiles. Document the density changes meticulously. This isolation process proves whether the defect stems from chemistry or machinery. Complete this evaluation before committing to heavy capital expenditure.
Resolving uneven density requires a comprehensive, holistic approach. You must understand the complex interplay between formulation mixing, extruder health, and thermal calibration. Attempting to fix a mechanical problem by tweaking a chemical recipe leads directly to frustration and wasted capital. Machinery degradation, particularly in screws and die heads, fundamentally disrupts melt flow.
We strongly recommend starting with a rigorous audit of your mixing procedures. Verify your powder homogeneity first. Next, calibrate your die head and inspect your cooling tables. Eliminate process errors before escalating to major equipment replacement. If data proves your machinery can no longer maintain strict tolerances, upgrade decisively. Encourage your engineering team to consult technical equipment specialists today to audit your current production bottlenecks.
A: Adjusting the foaming agent alters the overall average density. However, localized unevenness rarely stems from a gross formulation error. Heavy edges or patchy voids almost always indicate a mechanical flow restriction, poor powder mixing dispersion, or uneven temperature distribution across the die head.
A: Inspection intervals depend entirely on your filler content. Formulations utilizing high percentages of calcium carbonate act as harsh abrasives. For highly filled recipes, inspect screw clearances every six months. Standard formulations typically allow for annual inspections during major preventative maintenance shutdowns.
A: High edge density typically points to a severe die temperature imbalance where the outer edges run too cold. It also frequently results from improper choker bar settings. If the center bar restricts flow excessively, the melt forces outward, packing the edges tightly.
A: Yes. Extreme cooling gradients within the calibration unit alter expansion rates dramatically. If the outer skin freezes instantly while the core remains excessively hot, the internal foam struggles to expand outward. This uneven thermal shock directly impacts overall panel thickness and structural density uniformity.